If you work in industries like oil & gas, chemical processing, power generation, or even water treatment, forged valves are probably one of those workhorse components you don’t think about until they stop working. I’ve been a forged valve supplier for over a decade, and let me tell you: smooth operation isn’t luck—it’s the result of choices we make before a valve even leaves our warehouse, and the stuff clients do after it’s installed. A lot of folks reach out to me asking how to keep their forged valves running without unexpected shutdowns, so I wanted to break this down in real, no-fluff terms—nothing too tech-jargon heavy, just what actually works in the field. Forged Valves
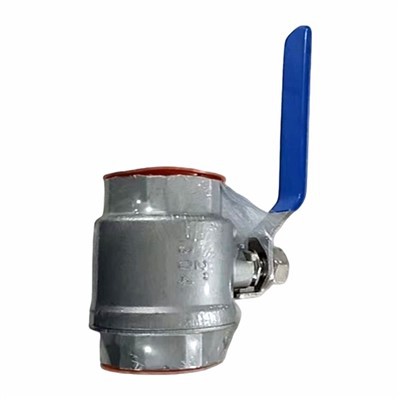
First off, let’s get one thing straight: forged valves are built to last, but their reputation for durability only holds up if you don’t skip the basics. I’ve seen clients install top-of-the-line forged globe or gate valves from reputable brands, then have them fail in half the expected time because of tiny, avoidable mistakes. The first step to ensuring smooth operation starts with selecting the right valve for the job. It sounds obvious, but you’d be shocked how many people pick a valve based on price alone or a vague “it’s a forged valve” label, not the actual application demands.
Let’s talk material specs for a sec—this is non-negotiable. Forged valves come in all sorts of alloys: carbon steel, stainless steel, duplex, even specialty materials like Monel or Hastelloy. If you’re moving highly corrosive chemicals, using a basic carbon steel forged ball valve is a disaster waiting to happen. I had a client a couple years back who installed a carbon steel forged valve for a 20% sulfuric acid line, thinking “forged is forged, right?” Within six months, that valve was leaking so bad they had to shut down their entire processing unit. We swapped it for a forged duplex stainless steel valve, and that same valve has been running for eight years with zero issues. The key here is matching the valve’s body material, trim (the internal parts that touch the fluid), and seal materials to the process media, temperature, and pressure. Don’t let a sales rep pressure you into a one-size-fits-all approach—ask for the exact corrosion resistance ratings, pressure-temperature (P-T) charts, and make sure they align with your specific line.
Next up: the design and manufacturing checks that happen when a valve is being made. As a supplier, this is where I pour most of my energy, because cutting corners here sets everyone up for failure. Forged valves get their strength from the forging process itself—beating or pressing metal into shape under high pressure, instead of casting it, which leaves weak spots and porosity. But even with forging, not all processes are equal. We do full heat treatment on every valve we make—no exceptions. Skipping heat treatment leaves residual stress in the metal, which can cause cracking when the valve is exposed to thermal cycling or high pressure. I’ve visited a plant where a competitor’s un-heat-treated forged gate valve split open during a hot startup, releasing superheated steam and shutting down production for three days. That mistake would have cost the client way more than choosing a reputable supplier who does proper heat treatment.
Also, pay attention to the valve’s trim and sealing components. A lot of cheap forged valves use generic rubber or plastic seals that break down fast in extreme temps or caustic fluids. We use PTFE, Kalrez, or metal seals depending on the application, and we test every valve’s bubble-tight integrity before it leaves our facility. That pressure test isn’t just a box to tick—It’s how you catch a faulty weld, a misaligned seal, or a small forging defect that would lead to leaks or stuck valves later. If your supplier doesn’t offer a detailed test report with every valve, keep looking. That report is proof the valve can handle what you’re going to throw at it.
Once the valve arrives at your facility, proper storage and handling are make-or-break. I can’t tell you how many times clients tell me their forged valves stopped working just because someone dropped them, or left them sitting outside in the rain for weeks. Forged metal is strong, but the internal seals, stem threads, and sealing surfaces (like the valve’s seat) are delicate. If you drop a valve, even if it doesn’t look damaged, it can shift the internal trim, making the stem hard to turn or causing leaks. And moisture? Even a tiny bit of rust on the stem can cause it to seize up over time, especially if the valve isn’t operated regularly. We always deliver valves in crates with protective caps on the inlet/outlet ends, and we recommend clients store them in a dry, temperature-controlled area, off the ground, with stems protected from dirt and moisture. If you have to store a valve long-term, lubricate the stem and close it slightly (not fully tight) to keep pressure off the seals—another small step that makes a huge difference.
When it’s time to install the valve, skip the shortcutting here. I’ve seen techs use too much pipe dope on the threads, or over-torque the bolts on the valve’s body flanges. Over-torquing can crack the valve’s body or distort the flange, leading to leaks. Too little torque, and the joint will loosen from vibration during operation. We always give clients a torque spec sheet with every valve, specific to the size and material—follow it. Also, make sure the valve is installed in the right direction. Most forged valves have an arrow on the body showing the flow direction; installing it backwards doesn’t just hurt performance, it can cause excessive wear on the trim and make the valve harder to operate. A client once installed a forged check valve backwards, thinking “flow is flow,” and within a month, the check valve was worn out because the internal disc was slamming the wrong way every time the flow reversed.
Now, the stuff after installation: regular maintenance. Forged valves don’t need daily inspections like a car, but they do need scheduled check-ins. Most of the time, small issues turn into big failures because they’re ignored. What does good maintenance look like? First, operate the valve regularly—even if it’s a valve that only gets turned on once a year, open and close it a quarter turn every few months to keep the stem moving smoothly. Seized stems are one of the most common complaints I get, and 90% of the time it’s because the valve hasn’t been operated in months.
Second, lubricate the stem and packing area as recommended by the supplier. Too much lubricant will attract dirt and cause buildup, too little leads to friction and wear. For forged valves, we use a high-temperature, pressure-resistant lubricant that works for most industrial applications, but we adjust if the client has extreme conditions. Also, check for leaks around the stem, flanges, and body during routine shutdowns. A small drip today can turn into a major leak during a pressure spike, which is way more expensive to fix.
Third, keep an eye on the operating conditions. Things change over time: a line that used to carry clean water might now have small particulates, or the temperature might creep up higher than the original P-T rating. If that happens, don’t just keep running the same valve—reach out to your supplier. We’ve had clients adjust a valve’s trim or change out the seals to match updated process conditions, saving them from having to replace the entire valve. It’s way cheaper to modify a forged valve that’s already working for you than to buy a brand new one.
I also want to bust a common myth: forged valves don’t need regular testing, right? Wrong. Periodic testing of valve performance is critical, especially in high-risk industries. For example, in oil & gas, testing the valve’s shut-off capability ensures it will work in an emergency. For chemical processing, checking for seat integrity prevents cross-contamination. We offer clients custom maintenance checklists tailored to their specific application, and most who use them cut their valve failure rate by 70% or more.
At the end of the day, ensuring forged valves run smoothly isn’t rocket science—it’s about being intentional at every step: picking the right valve for the job, working with a supplier that stands behind their manufacturing, storing and installing it correctly, and keeping up with basic maintenance. Too many people treat valves like a set-it-and-forget-it part, but that’s where things go wrong.
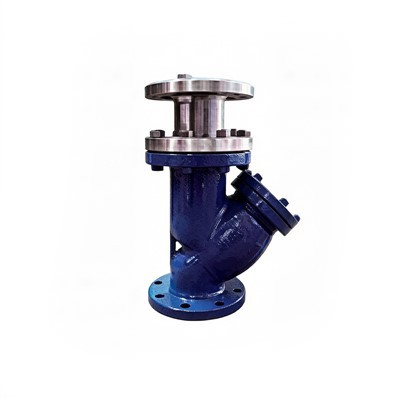
Y-type Filter If you’re dealing with forged valves that are acting up, or you’re planning a new project and need to make sure your valves keep your operations running, feel free to reach out to us for a no-pressure chat. We can walk you through selecting the right valve, share maintenance tips specific to your application, or answer any questions you have about our products.
References
- ASME B16.34, Valves – Flanged, Threaded, and Welded End
- API 600, Steel Gate Valves – Forged and Bolted-Bonnet
- Practical Maintenance of Industrial Valves, CRC Press, 2021
Xiongxiang Valve Group Co., Ltd.
As one of the most professional forged valves manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale cheap forged valves for sale here from our factory. Contact us for more details.
Address: Building 1, No.306, 12th Binhai Road, Jinkai District, Wenzhou City, Zhejiang Province, China
E-mail: info@xiongxiangvalve.com.cn
WebSite: https://www.steelvalvegroup.com/
